Calcined petroleum coke is often described as a commodity recarburizer. Buy on fixed carbon, check the price and you are done. That approach works for rebar and structural steels. It does not work for special grades.
The difference is not the carbon. It is what comes with the carbon. Every kilogram of CPC carries sulfur, nitrogen, vanadium and ash into the steel. For ordinary grades, those impurities disappear into the background. For bearing steels, HSLA grades or low-sulfur pipeline steels, they can determine whether the heat passes or fails.
This article looks at the impurities in CPC that matter most for special steel grades, how they affect steel quality and how to match the CPC specification to what you are producing. It assumes you already understand the basics of CPC handling. For a broader look at incoming inspection and general usage, see our article on calcined petroleum coke quality and use in steelmaking.
Why Sulfur Limits CPC Use in Special Steels
Sulfur is the impurity that most often limits CPC use in special steels. CPC sulfur content varies widely by source, from as low as 0.05% in premium grades to above 0.8% in lower-quality material. For a mill producing steel with a final sulfur specification of 0.005%, even a low-sulfur CPC contributes a measurable sulfur load.
The problem is cumulative. Sulfur from scrap, from alloys and from the recarburizer all adds up. If the CPC brings in 0.3% sulfur and you add 2 kg per ton, that is 6 grams of sulfur per ton of steel or roughly 0.0006% sulfur pickup. That sounds small, but for a heat already near the sulfur ceiling, it can be enough to push the steel out of specification.
Pipeline steels, bearing steels and any grade with a sulfur specification below 0.010% should be evaluated carefully before using standard CPC. The sulfur load may be tolerable if the starting sulfur is low and the addition rate is small. It becomes a problem when multiple heats in a sequence are pushing the limit.
Nitrogen Stays in the Steel
Nitrogen is more difficult to manage than sulfur because it is not removed in the ladle. Once nitrogen enters the steel, it stays there until vacuum degassing or other treatment removes it. That makes the recarburizer a nitrogen-control decision made at the purchasing stage, not in the melt shop.
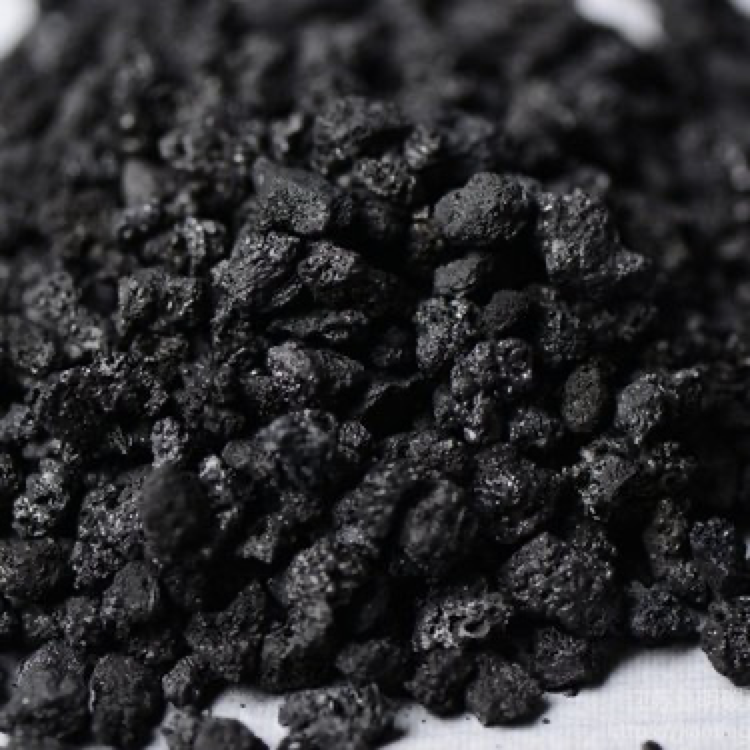
CPC nitrogen content typically ranges from 300 to 800 ppm, depending on the source and the calcination conditions. Some low-nitrogen CPC grades are available at 50 to 300 ppm. For ordinary carbon steels, that nitrogen contributes little. For drawing-quality steels, HSLA grades and any steel where strain aging or toughness matters, it can be significant.
The mechanism is straightforward. Nitrogen in steel forms aluminum nitride or other precipitates that pin dislocations and reduce ductility. It can also cause porosity and looseness in cast products. For a bearing steel or a cold-heading wire grade, nitrogen pickup of even a few parts per million can push the final chemistry out of specification. When your steel grade has a nitrogen ceiling below 80 ppm, standard CPC becomes difficult to justify. A low-nitrogen CPC or a switch to graphitized petroleum coke, which typically contains below 100 ppm nitrogen, is usually the better choice.
The Overlooked Risk of Vanadium and Other Metals
Sulfur and nitrogen get most of the attention. Vanadium and other residual metals in CPC are less discussed, but they matter for certain applications.
CPC contains small amounts of vanadium, nickel and iron, typically below 0.5% combined. For most steels, those metals are either harmless or beneficial. Vanadium is a strong carbide former and can increase strength. But for steels where vanadium is not specified, the extra vanadium from CPC changes the hardenability and the tempering response.
This is a particular concern for steels with tight limits on residual elements, such as certain forging grades or steels destined for welding without post-weld heat treatment. If the vanadium specification is strict, the CPC source matters. Ask the supplier for a metals analysis, not just the sulfur and nitrogen numbers.
Matching CPC Grade to Steel Grade
The practical question is not whether CPC is good or bad. It is which CPC grade fits which steel. Here is how the matching works in practice, with the caveat that your own specifications always take precedence.
Rebar, structural steels and ordinary carbon grades tolerate standard CPC without difficulty. At 98.5% fixed carbon, 0.3% to 0.5% sulfur, and 300 to 500 ppm nitrogen, the impurities are well within the tolerance of these steel specifications and the cost advantage of CPC is real.
When it comes to HSLA and drawing-quality steels, the nitrogen ceiling becomes the limiting factor. A low-nitrogen CPC with nitrogen below 300 ppm is preferred and the sulfur should be below 0.3% to avoid adding to the desulfurization burden.
For bearing steels, tire cord and cold-heading grades, standard CPC is usually not suitable because the sulfur and nitrogen limits are too tight. Graphitized petroleum coke or a premium low-impurity CPC is the safer choice. For a detailed comparison of when the premium for GPC is justified, see our article on graphitized petroleum coke or CPC when to pay more.
If your steel has tight limits on residual elements, such as certain forging grades or steels destined for welding without post-weld heat treatment, request a full metals analysis from the CPC supplier and verify the vanadium, nickel and iron content against your specification before the first shipment.
What to Request on the Certificate
For special steel applications, the standard CPC certificate is not enough. Ask for the following items on every lot.
Sulfur should be reported as a specific value, not a range. A certificate that says “sulfur: 0.3% max” tells you the ceiling, not the actual content. You need the actual number to calculate the sulfur load.
Nitrogen should also be a specific value. The difference between 200 ppm and 500 ppm nitrogen matters when your steel ceiling is 80 ppm.
Vanadium and other metals should be reported if your steel grade has residual limits. If the supplier cannot provide a metals analysis, that is a sign they are not controlling the source.
Ash and volatile matter should be reported because they affect slag volume and carbon yield. High ash CPC adds slag that you have to manage and high volatile matter means the fixed carbon number is lower than it appears.
When CPC Is Not the Right Answer
CPC is the economical choice for the majority of steel grades. But for a meaningful minority, it is the wrong tool. Recognizing those cases saves you from quality problems that are difficult to trace back to the recarburizer.
If your steel grade has a sulfur specification below 0.010%, a nitrogen ceiling below 80 ppm or tight limits on residual metals, evaluate whether CPC can meet the requirement before committing to a shipment. If it cannot, the premium for GPC or a low-impurity recarburizer is usually cheaper than the cost of a rejected heat.
We supply CPC in a range of sulfur and nitrogen specifications and can help you match the grade to your production requirements.
If you have any needs, please contact us without any hesitation!